Superabrasive fusion-bonding technology
Based on over 10 years of research on diamond and cubic boron nitride (CBN) interface wettability, the "superabrasive fusion-bonding" process chemically bonds superabrasives to metal substrates for precision machining under extreme conditions.
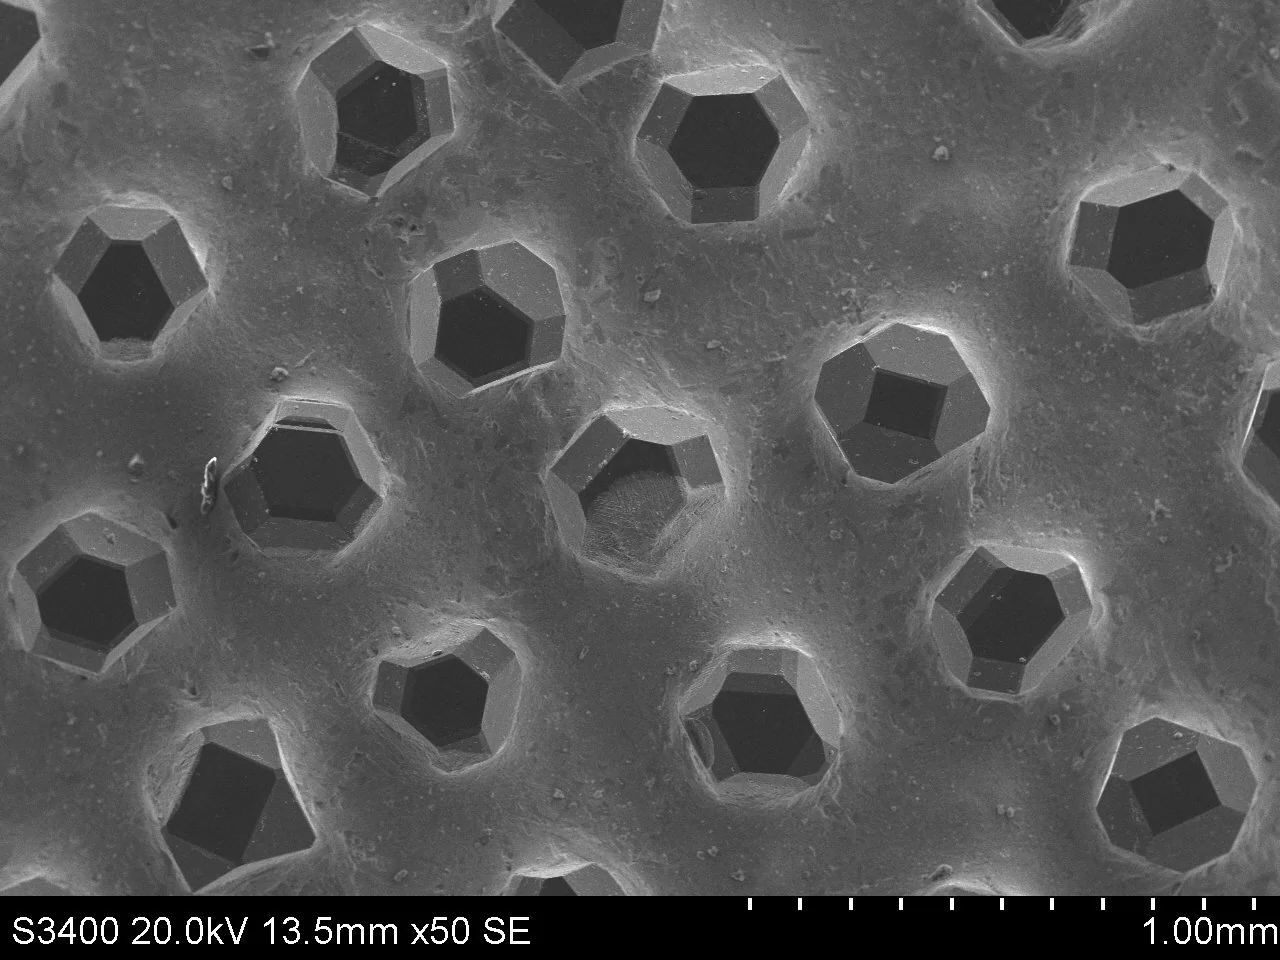
Core capabilities
From interface modification to systems engineering, building the underlying technical foundation of the sp³–sp² platform
Interface modification & bonding
Focused on solving the bonding challenge between superabrasives (Diamond/CBN) and heterogeneous substrates, using active fusion bonding (Active Fusion-Bonding) to form high-strength interface compounds for atomic-level chemical bonding.
Extreme condition adaptation
Providing customized cutting/grinding solutions for "difficult-to-machine materials" such as aerospace superalloys, carbon fiber composites (CFRP), and ceramic matrix composites (CMC), ensuring process stability and efficient machining.
Technology downward compatibility
Translating industrial-grade precision control into underlying process specifications supporting sp³–sp² consumer products (e.g., diamond nonstick coating) and industrial thermal management (diamond-copper), enabling continuous technology evolution.
Product design principles: Three-element architecture of superabrasive fusion bonding
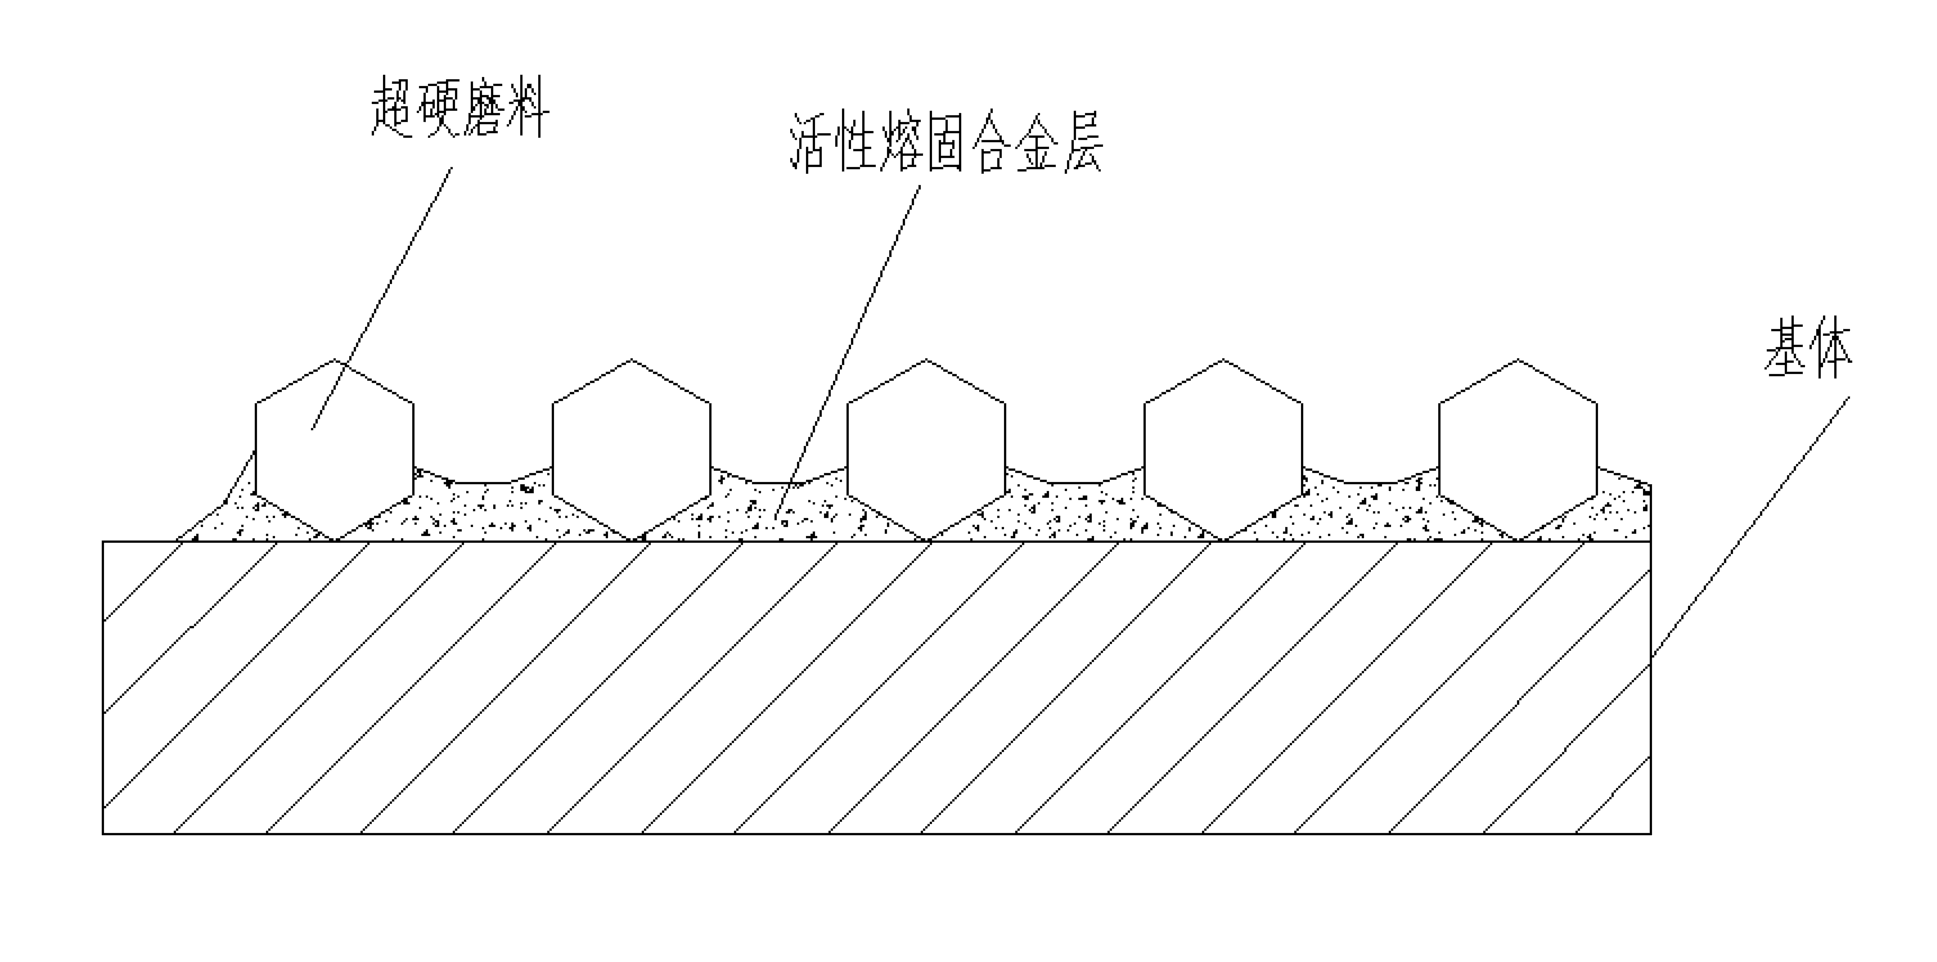
Performance of active fusion-bonded superabrasive tools is determined by three core elements: Substrate, Superabrasive, and Active fusion alloy
Substrate
As the abrasive carrier, provides structural support and rigidity for the tool through geometric conformal adaptation to specific machining conditions.
Superabrasive
As micro-cutting tools, undertake material removal (Diamond/CBN), determining tool cutting capability and service life.
Active fusion alloy
As the bonding link, determines overall tool service performance through chemical metallurgical reactions; the key control point for performance.
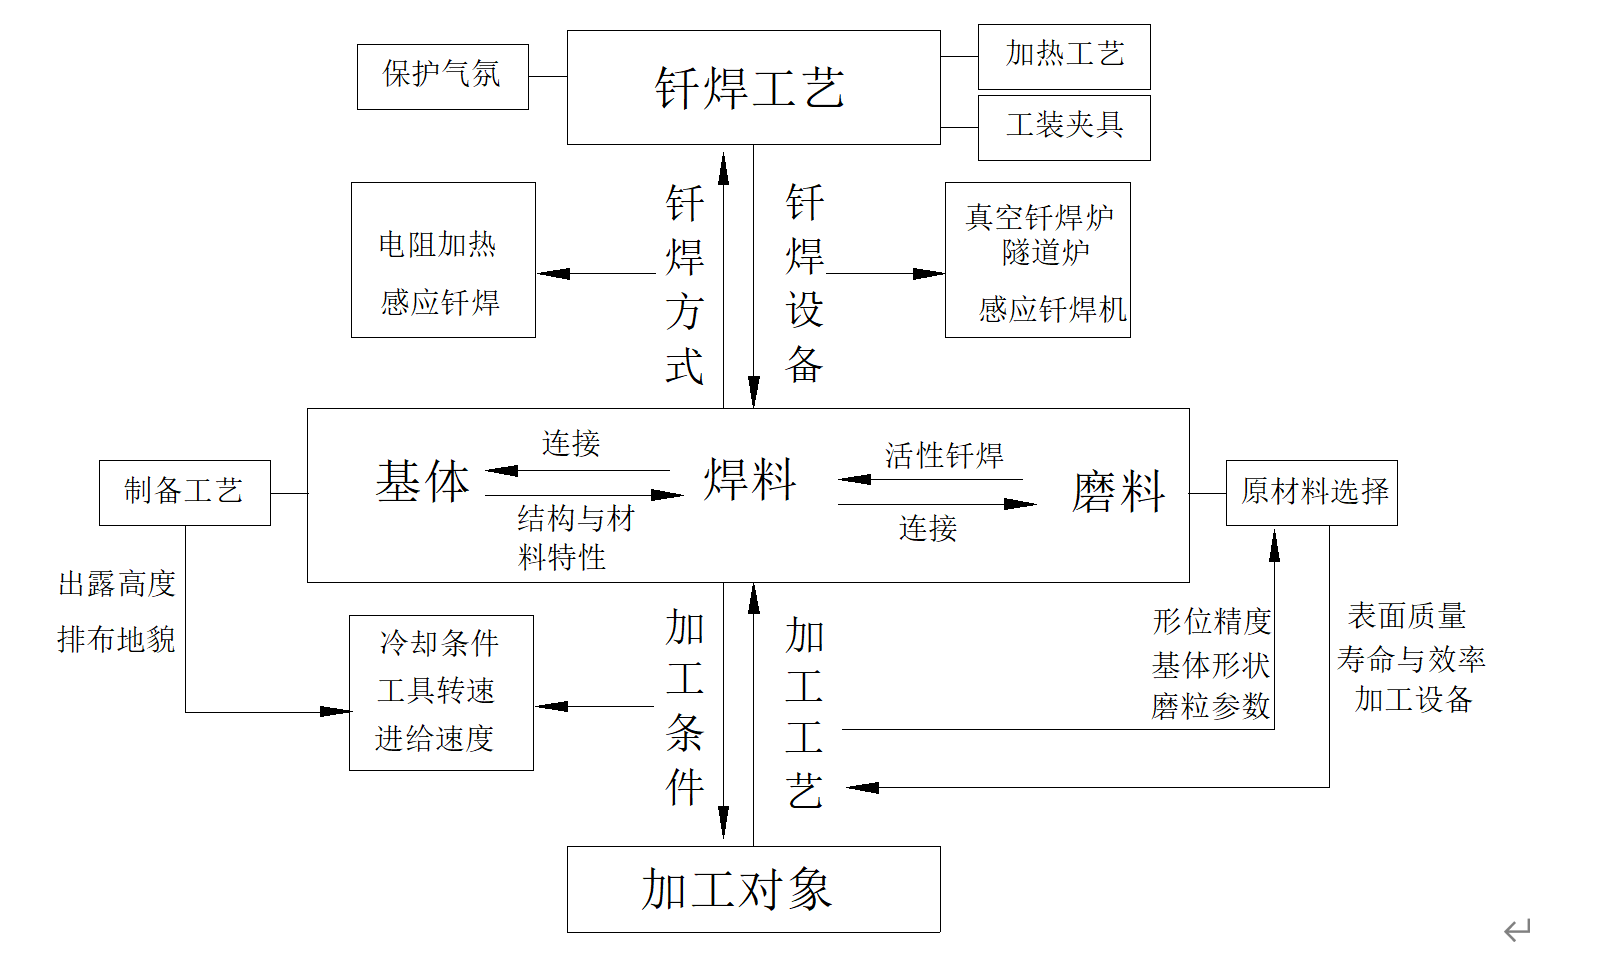
System design logic
Tool design is not element stacking but optimization across machining object (superalloys, composites) and conditions (dry/wet cutting), matching four dimensions — substrate, abrasive, placement, and fusion atmosphere.
Engineering support under extreme conditions
In aerospace, semiconductor manufacturing, defense, and other fields, difficult-to-machine materials impose stringent requirements on tool reliability
Ceramic matrix composite (CMC)
Core material for aero-engine hot-section components; extremely difficult to machine, demanding high wear resistance and thermal stability from tools.
Carbon fiber composite (CFRP)
Mainstream material for aerospace structures and new energy vehicle bodies; prone to delamination and burrs during machining, requiring precise cutting control.
Titanium alloy (Ti-6Al-4V)
Key material for aerospace and medical devices; generates high heat during machining, posing dual challenges for tool heat dissipation and strength.
Solution value
The solution provides not only tools but also material-matched machining process specifications. Through superabrasive fusion-bonding technology, chipping, thermal damage, and efficiency bottlenecks in machining high-value complex parts are addressed.
Process specification output
- Complete cutting parameter recommendations (speed, feed, cooling method)
- Tool selection guide for specific materials
Full lifecycle support
- On-site technical support and process optimization
- Tool performance tracking and continuous improvement
Active fusion-bonding technology deep dive
Superabrasive active fusion-bonding principle
Active Fusion-Bonding Technology
In ultra-clean vacuum or controlled atmosphere, customized fusion alloys drive atomic-level bonding with the surfaces of superhard materials (diamond, CBN, PCD) — not mere physical connection but deep atomic coupling, building high-strength, low-resistance integrated structures.
Precisely controlled by alloy system
Effectively suppresses component volatilization, ensures fusion layer density
Core advantages: four-dimension comparison
High-strength chemical bonding
Fusion alloy optimized for superhard materials; achieves extremely high bonding strength while avoiding excessive erosion, fully preserving physicochemical properties of superabrasives.
Physical property assurance
Vacuum environment not only prevents oxidation but, through negative pressure precision control, ensures fusion alloy composition stability, achieving excellent tool surface cleanliness and consistency.
High grain protrusion
Compared to electroplating and traditional brazing, active fusion-bonding gives stronger grain exposure, more cutting edges, significantly improving material removal rate.
Precision machining adaptation
Fusion alloy uses atomization and multi-stage screening; precisely paired with different abrasive specifications, excellent surface consistency, designed for precision and ultra-precision machining.
Key material systems
- • High-grade synthetic diamond
- • Cubic boron nitride (CBN)
- • Polycrystalline diamond (PCD)
- • High-performance atomized active alloy powder
- • Adapts to various complex fusion processes
- • Multi-stage screening for precise pairing
- • Stainless steel
- • High-strength alloy steel
- • Low-carbon alloy steel and other engineering materials
Application domain upgrade
Active fusion-bonded tools are widely used in:
Hard brittle / ferrous metals
- • Superhard ceramics
- • High-strength steel
- • Ductile cast iron
Advanced composites
- • CFRP (carbon fiber reinforced composite)
- • Glass-ceramic
- • Composite panels
High-end manufacturing
- • Aerospace component machining
- • New energy precision structural parts
- • Marine and heavy equipment
Technology migration: From "interface bonding" to "all-carbon platform"
How the core principle of superabrasive fusion-bonding evolves into the sp³–sp² all-carbon composite platform
Origin
Superabrasive active fusion mechanism—achieving chemical bonding between Diamond and metal, breaking through performance limits of traditional physical setting.
Extension
Diamond-copper combination—through high-strength, low-thermal-resistance interface, building diamond-copper heat spreader substrates, entering thermal management.
Expansion
sp³ diamond and sp² carbon material homogeneous-heterogeneous bonding—breaking metal limits, building all-carbon composite platform, exploring physical computing potential.
Need professional machining solutions?
The engineering team has 10+ years of superabrasive tool R&D experience and provides customized technical consultation